English
 Español
 Português
 Français
 Deutsch
 русский
 한국어
 にほんご
 हिन्दी, हिंदी
 বাংলা
 Bahasa Indonesia
 Türkçe
 Việt
 dansk
 čeština
 עִבְרִית Ivrit
 Filipino/Pilipino
 български език (Bǎlgarski jazik)
 suomi
 norsk
 język polski
 ไทย
 ກະຣຸນາ
 Bahasa Melayu
 ភាសាខ្មែរ
 ဗာရမ်
 اردو
 فارسی
 Italiano
 Nederlands
 svenska
 Монгол хэл
 नेपाली
 සිංහල
 Ўзбек тили
 پښتوتۆرکجه
 Ελληνικά
 српски / srpski
 magyar
 українська
 Kiswahili
 Қазақ тілі
 Română
 Hrvatski
 Bosanski
 Kreyòl ayisyen
 አማርኛ
 Hausa
 Yorùbá
 Igbo
Should a bulk barrier order include a pre-shipment inspection?
A bulk barrier order should usually include a pre-shipment inspection, particularly when the barriers will control access around electrical equipment. A shipment can match the invoice yet arrive with incompatible connectors, unstable bases, missing warning signs, or packaging that leaves panels vulnerable to damage. Finding these issues before dispatch gives the buyer an opportunity to require correction before freight and site schedules become involved.
The inspection scope matters more than a simple pass stamp. Retractable belts, portable fences, rigid screens, and insulating barriers do not provide the same protection. A visual inspection can confirm workmanship, dimensions, assembly, and labeling; it cannot establish a dielectric rating. The practical decision is therefore not just whether to inspect, but which checks and supporting test records the order requires.
Start by defining what the barrier is supposed to do
Before comparing inspection options, separate access control from electrical protection. A warning barrier may help keep unauthorized people outside a designated work area without being designed to prevent electric shock. An insulating barrier intended for a specified electrical application requires different technical evidence and acceptance criteria.
This distinction becomes important when a purchase description uses broad terms such as “electrical safety barrier” or “insulated fence.” Neither phrase, by itself, establishes an electrical rating. Even a nonmetallic structure may contain conductive fittings or have no verified dielectric performance.
The purchase specification should identify:
- Intended function: visual warning, restricted access, physical separation, or a defined insulating application.
- Configuration: panel dimensions, extended belt length, base type, connection method, and required accessories.
- Use conditions: indoor or outdoor placement, expected ground conditions, storage arrangements, and relevant environmental exposure.
- Required evidence: approved drawings, material documentation, applicable test reports, and any specified product markings.
Inspection then checks the shipment against that agreed specification. It should not be used to resolve an undefined safety requirement after production is complete. Where electrical protection is claimed, the responsible technical person should confirm the applicable requirements before the order is released for manufacture.
Factory checks, independent inspection, or arrival inspection?
These options serve different purposes. Supplier quality control should operate throughout production. A buyer-appointed pre-shipment inspection provides another verification point before dispatch. Arrival inspection checks what actually reaches the warehouse or site, including possible transit damage.
For an established, unchanged access-control product, documented factory checks may justify reducing independent inspection frequency. That decision should reflect actual quality history, not familiarity alone. A material substitution, revised connector, new production location, or recurring packaging complaint is a reason to increase verification again.
Independent inspection is especially useful when multiple barrier variants look similar. Different heights, sign languages, base weights, or connection details can be mixed during packing even when individual components appear well made.
The inspection scope should follow the likely failure points
Identity, quantity, and compatibility
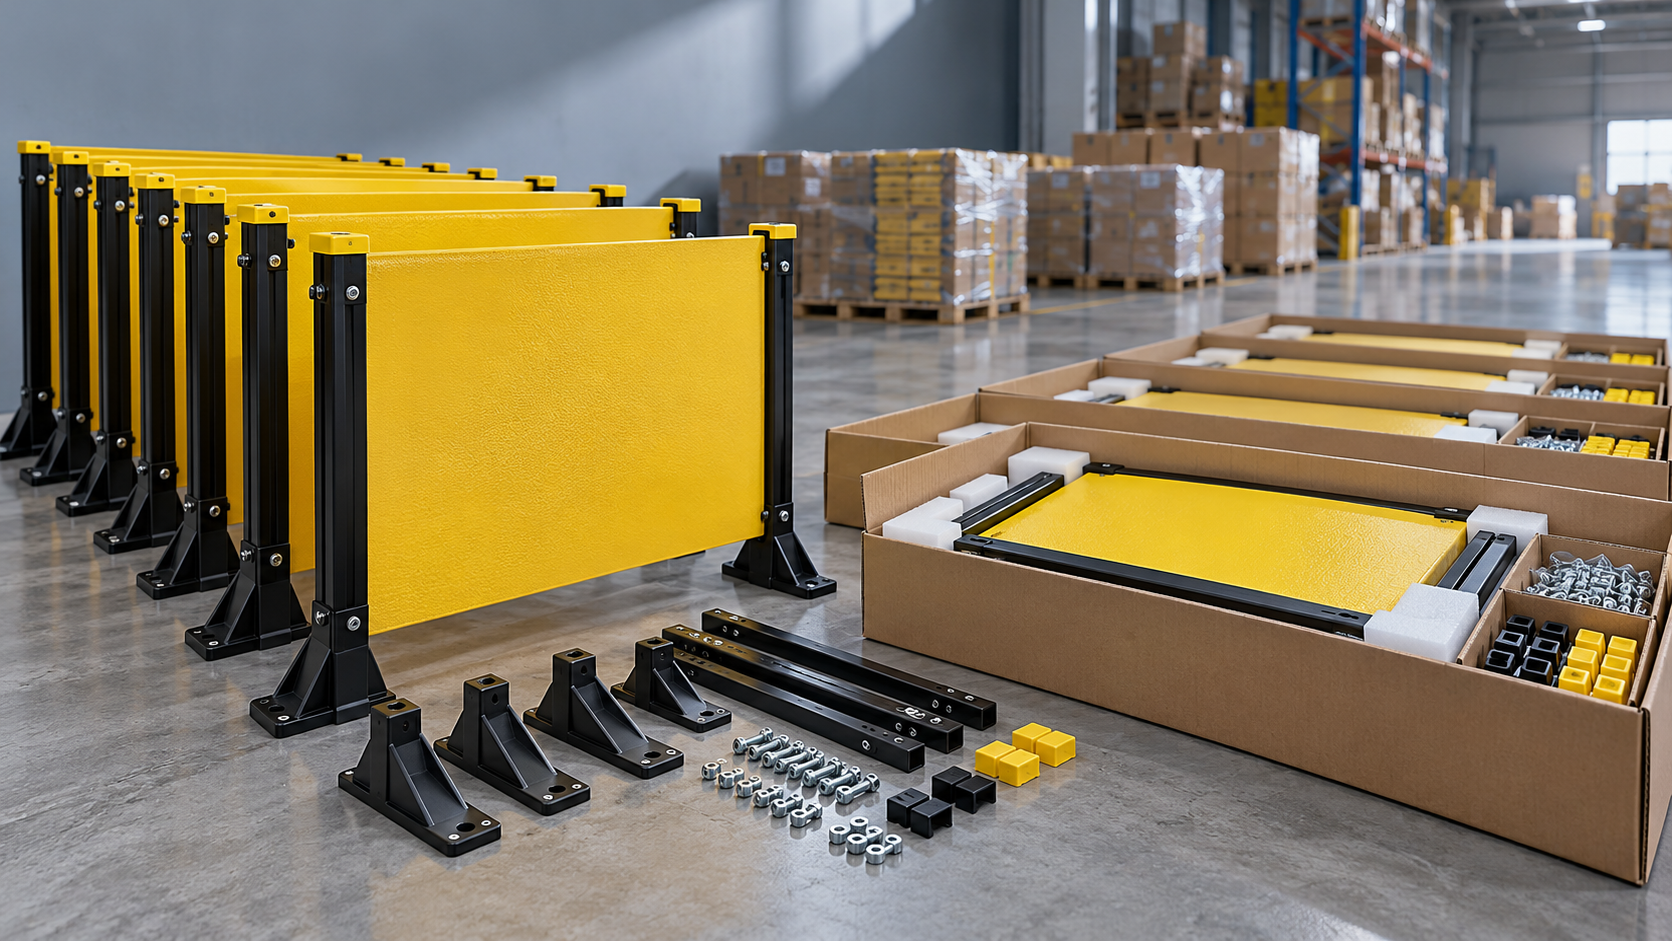
Start with model references, purchase-order revisions, quantities, and carton identification. Confirm whether “one set” means a complete usable assembly or a single component. A count of panels alone will not reveal a shortage of feet, clips, connecting chains, signs, or carrying accessories.
Assemble representative units using the supplied components. Check that adjacent panels connect correctly and that any specified compatibility with existing equipment is supported by approved interface dimensions or a suitable reference item. Components can each meet their own drawing while still failing to form the intended layout.
Mechanical condition and normal operation
Inspect edges, joints, fasteners, surface finish, and accessible moving parts. Look for cracks, distortion, loose fittings, exposed sharp edges, and damage around fixing points. On retractable barriers, verify normal extension, latching, and controlled retraction according to the manufacturer’s instructions.
Portable units should stand and connect as specified on a suitable test surface. Check base engagement, locking arrangements, and the assembled footprint. An informal push test cannot establish wind resistance or suitability for uneven outdoor ground; those claims need defined criteria and appropriate evidence.
Where folding joints or adjustable sections are present, operate them through their intended range. Binding, unintended release, or excessive looseness can make a barrier difficult to deploy consistently, even when its appearance is acceptable.
Warning information and packaging
Check sign wording, language, symbols, orientation, and attachment against approved artwork. Confirm that product identification and any required limitations remain legible after assembly. A general warning sign must not be mistaken for evidence of an electrical protection rating.
Packaging deserves a separate review. Heavy bases should not move against panels or mechanisms during handling. Protective separators, restrained components, suitable cartons, and clear packing identification can reduce the risk of rubbing, bending, and loose hardware. Where moisture exposure is foreseeable, review the agreed packaging provisions rather than assuming ordinary wrapping is sufficient.
Electrical claims need more than a visual pass
A pre-shipment inspection report is not proof of electrical insulation performance unless the relevant testing is explicitly included and properly performed. Appearance, color, and material descriptions cannot establish a safe working voltage or suitability for a particular electrical task.
For barriers sold with a defined electrical protection claim, request documentation that identifies the product tested, the applicable test method or standard, the test conditions, and the results. Check whether the report covers the supplied construction and configuration. A report for a raw material or a different model may not substantiate the finished barrier’s claimed performance.
Keep the different forms of evidence separate:
- Design or type-test evidence supports the performance of an identified design under stated conditions.
- Routine production records document specified checks performed during manufacture, where applicable.
- Shipment inspection results describe the goods examined and the checks completed for that order.
Traceability should connect the delivered model and relevant batch information to the records required by the contract. The necessary depth depends on the product and its intended protective function; not every access-control barrier requires dielectric testing.
Do not add improvised high-voltage testing to a general inspection visit. Electrical tests require suitable equipment, controlled conditions, competent personnel, and an agreed procedure. Some tests may damage products or require particular sample handling. Define those requirements before production, including whether tested samples can be supplied.
Agree on sampling and defect decisions before inspection day
“Inspect before shipment” is too vague to produce a dependable release decision. The inspection instruction should identify the order quantity, product variants, sampling method, checks to perform, and acceptance rules. Where a recognized acceptance-sampling plan is used, state its parameters and how defects will be classified.
Sampling should represent the shipment rather than a prepared display. The inspector should be able to select units from different cartons and relevant production lots. Mixed orders need coverage across configurations; a large sample of one model does not verify another model packed alongside it.
Classify defects by their consequence and intended use. An incorrect safety marking, a failed connection that defeats the intended boundary, or missing required protection evidence should not be treated like a minor cosmetic blemish. The contract should define release-blocking conditions and distinguish them from repairable or acceptable appearance variations.
For safety-critical requirements, a general sampling acceptance result may not be enough. Specify which features require full verification, which need documented production checks, and which can be sampled. Even full inspection has limits, so the inspection plan must remain part of a broader quality process rather than replace it.
Agree on measurement methods too. Dimensions need reference points and tolerances; functional checks need a defined procedure. Instructions such as “strong construction” or “good quality” leave too much room for disagreement between the buyer, factory, and inspector.
Schedule the inspection while correction is still possible
A pre-shipment inspection is most useful when the goods are complete and sufficiently packed to assess the actual shipping configuration, but still accessible for examination. The required production and packing status should be agreed with the inspection provider and supplier in advance.
Build time for corrective action into the dispatch plan. Booking an inspection immediately before collection can turn a quality decision into a freight deadline dispute.
- Before production: approve specifications, drawings, markings, documentation requirements, and acceptance criteria.
- Before the visit: confirm production readiness, packing status, available records, and access to the shipment.
- During inspection: record sample identity, measurements, assembly results, defects, and packaging condition.
- Before dispatch: review findings, verify any corrections, and issue release through the authorized purchasing process.
For substantial rework, request reinspection rather than relying only on selected photographs. A photograph may confirm that a missing label was added, but it may not establish that every affected carton was corrected or that repaired mechanisms operate properly.
Make release decisions from the findings, not the report label
A useful report identifies the inspected shipment, sampling coverage, checks performed, and any limitations. Photographs should support specific observations. “Passed visual inspection” is insufficient when the order also required assembly checks, dimensions, document review, or verification of accessories.
Separate straightforward corrections from unresolved technical questions. Replacing damaged packaging or adding omitted accessories may allow release after verification. An unsupported electrical rating, unapproved material change, or unexplained functional failure needs technical review before the affected goods are accepted.
The buyer should retain release authority unless the contract assigns it elsewhere. Supplier agreement that a defect is minor does not settle whether it is acceptable for the intended application.
For most bulk barrier purchases, the practical choice is supplier quality control supported by a risk-based pre-shipment inspection and a receiving check. Allocate inspection effort where it changes the decision: configuration accuracy, complete assemblies, dependable operation, protective packaging, and evidence for any claimed electrical performance. After delivery, confirm shipment identity and transit condition; a satisfactory factory inspection does not establish that the barriers arrived undamaged or are suitable for every site layout.
Recommend
 Oct 26, 2026
Does Grape Kool-Aid Repel Birds? Evidence and Risks for Garden Use
Does grape Kool Aid repel birds? Explore the evidence, plant and wildlife risks, and more reliable garden protection options. Find out what works before you spray.
- Oct 26, 2026
How to Hang Bird Repellent Tape on Roof Edges Without Loose Strips
Learn how to hang bird repellent tape on roof edges without loose strips. Get practical tips on secure mounts, spacing, and electrical safety for a cleaner, safer installation.
- Oct 25, 2026
Homemade Bird Repellent Spray: Recipe Limits and Outdoor Surface Risks
Searching for how to make homemade bird repellent spray? Discover recipe limits, outdoor surface risks, electrical safety tips, and safer deterrents before you spray.